Why Thread Machining Deserves Its Own Playbook
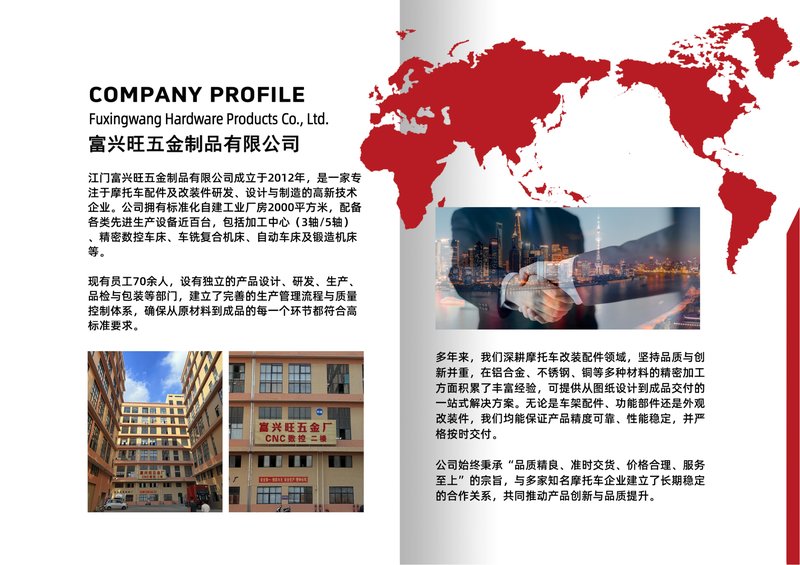
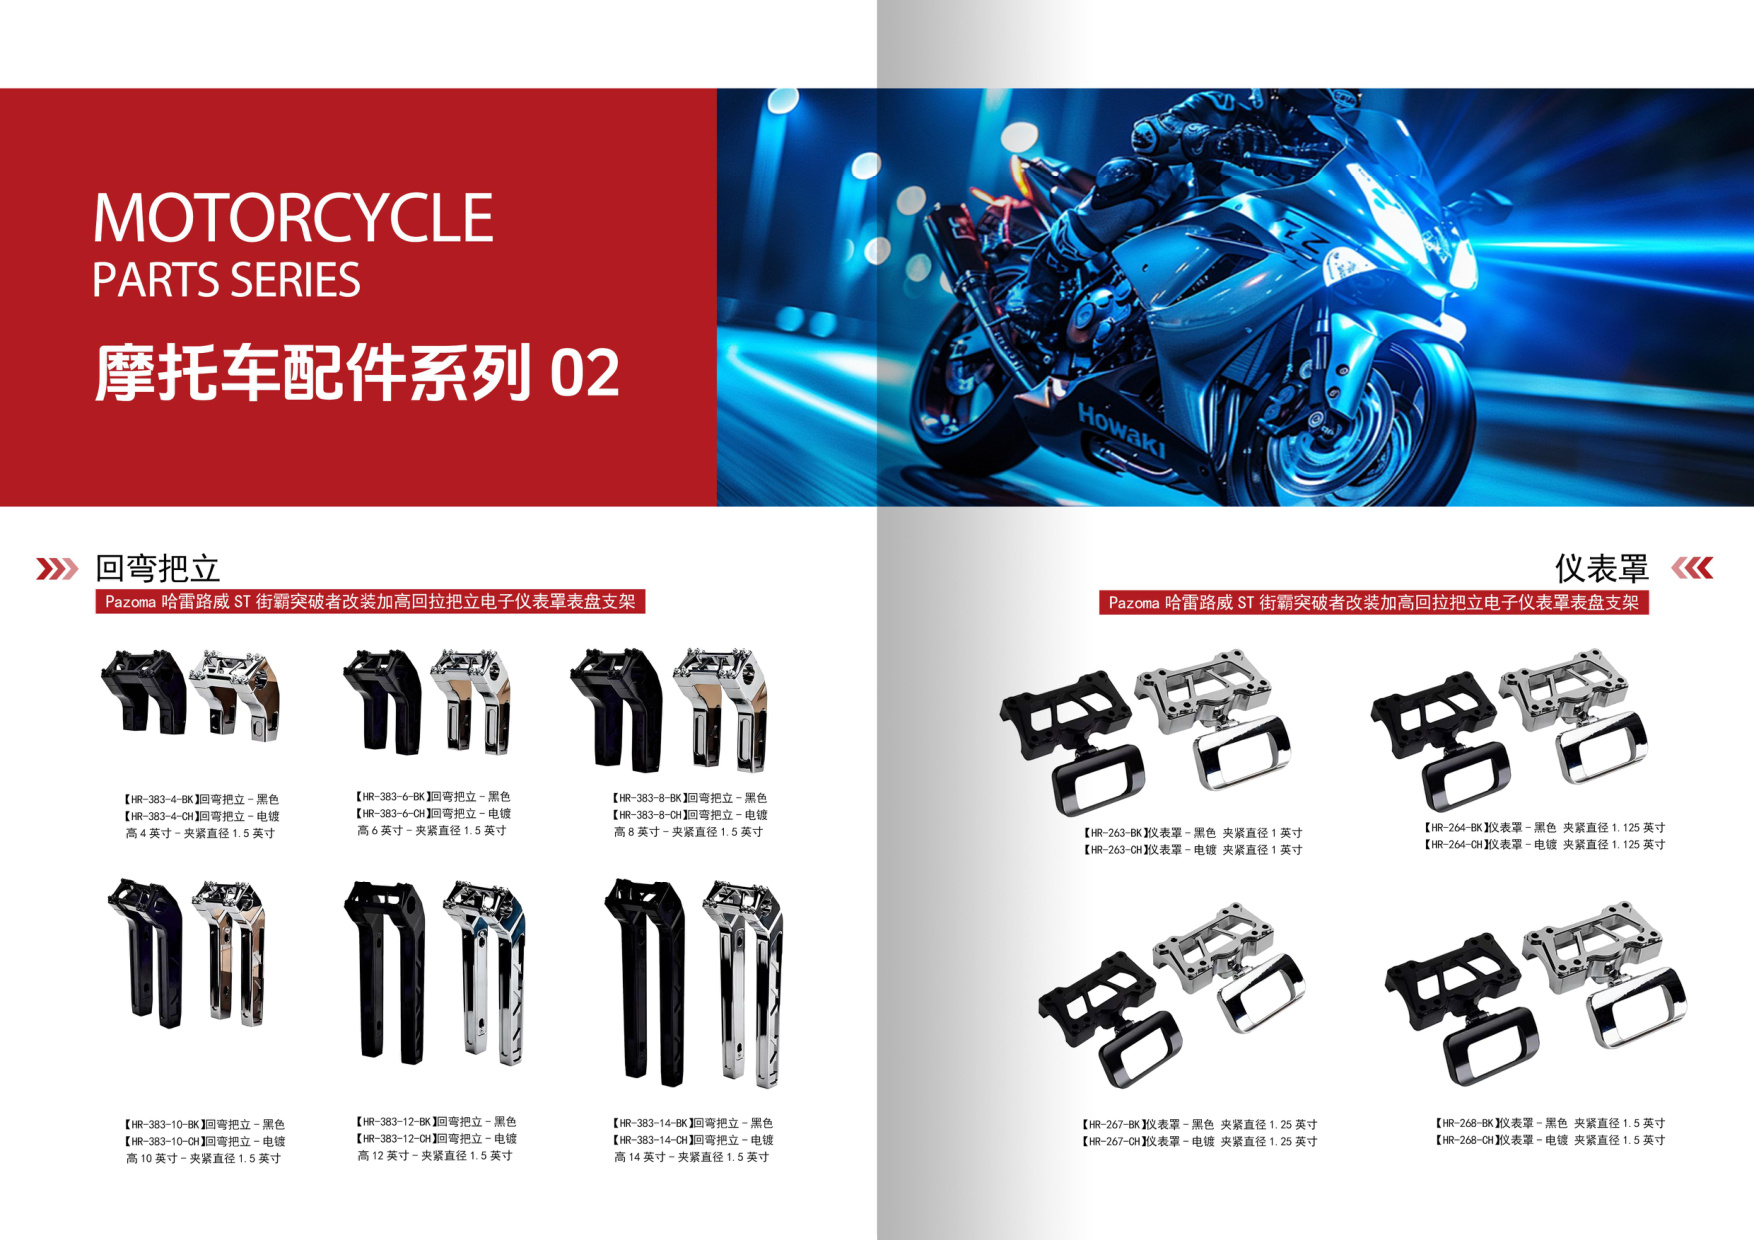
In CNC machining, threads are small features with outsized consequences. A single mis-pitched or torn thread can scrap an otherwise perfect part, delay an assembly line, or cause a field failure in a motorcycle brake caliper mount. At Fuxingwang Hardware Products Co., Ltd. (Jiangmen Fuxingwang Hardware), a motorcycle parts manufacturer founded in 2012, we cut threads on everything from aluminum engine covers to stainless steel axle nuts. After years of producing precision CNC parts on more than 100 CNC machines in our 2,000 sqm factory, we have collected a set of practical notes that help buyers and machinists get threads right the first time.
Thread Milling vs. Tapping: Choose by Material and Risk
When thread milling wins
Thread milling uses a rotating cutter on a helical path. It is our default for large-diameter threads (above M12), hard materials, and any thread close to a shoulder or thin wall. Because the cutter engages intermittently, chip evacuation is easier, tool pressure is lower, and a broken cutter does not leave a tap stuck in the hole. On precision CNC parts such as fork caps and shock mounts, thread milling also lets us adjust the minor diameter with cutter compensation, which keeps gauge fit consistent across a production run.
When tapping still makes sense
For small threads (M2–M8) in aluminum and brass, rigid tapping on a CNC machine is fast and repeatable, especially with synchronized spindles and thread-forming taps. Forming taps displace material instead of cutting it, producing stronger threads with no chips. The trade-off: hole size must be tightly controlled, and the material must be ductile. On hardened steel or cast iron, cutting taps with the right coating remain the safer choice.
Notes on Pitch, Fit, and Class of Thread
Match the thread class to the function
Not every thread needs a 6H fit. For motorcycle parts, we often see three cases: fasteners that must not loosen (slightly tighter fit), adjustment threads that will be turned often (looser fit for anti-seize), and threads that receive plating. Plating adds thickness, so we cut pre-plate threads to account for it; otherwise a 6H hole becomes a 5H hole after zinc or nickel plating and the bolt will not enter.
Control the minor diameter, not just the pitch
Pitch diameter is what gauges measure, but the minor diameter drives tap load and thread strength. On blind holes, we drill deep enough to leave at least three to five free threads below the tap, and we program peck tapping for deep holes to clear chips. For custom CNC machining China projects with unusual thread callouts, we confirm the standard (ISO metric, UNC/UNF, BSP, NPT) and the gauge type before cutting metal.
Tooling and Setup Details That Pay Off
Rigid tapping parameters
Synchronize spindle speed and feed exactly; any mismatch shows up as thread flank damage. We keep tapping speeds conservative in stainless steel and use a tapping fluid rather than general coolant for gummy aluminum alloys. For thread milling, a single-form cutter covers a pitch range, which reduces tool changes on mixed batches.
Fixturing and access
Threads near a shoulder need clearance for the tap holder or cutter shank. We check this at the CAM stage, not at the machine. On long shafts, we support the workpiece to prevent vibration, which otherwise produces chatter marks on thread flanks and fails go/no-go gauges.
Inspection: Gauges Plus a Second Check
Go/no-go plug and ring gauges are the baseline. We also inspect thread flank finish under magnification on critical precision CNC parts, and we verify thread depth and chamfer on first articles. For high-volume motorcycle parts, we log gauge results per batch so trends show up before a nonconformance does. A clean 45-degree chamfer at the thread entry is not cosmetic; it guides the fastener and prevents cross-threading during assembly.
Common Failure Modes and Fixes
Torn or galled threads
Usually caused by insufficient lubrication, dull tools, or wrong cutting speed in stainless. Fix: fresh tool, dedicated tapping fluid, reduced speed.
Oversized or bell-mouthed holes
Often from chatter or a worn tap. Fix: shorten tool overhang, support the part, replace the tap and re-qualify the hole size.
Thread runout
Results from poor fixturing or a misaligned pre-drill. Fix: drill and tap in the same setup where possible, and verify spindle alignment.
Working With a Thread-Focused CNC Partner
Good threads come from specification, tooling discipline, and inspection habits, not from luck. As a motorcycle parts manufacturer and custom CNC machining China supplier, Fuxingwang Hardware handles metric and imperial threads, plating allowances, and gauge-verified batches from prototype to production. If your drawings include critical threads, send them over: our engineering team will review the callouts, flag any fit or plating risks, and return a free quote with lead time and inspection plan.
Ready to get started? Email your 2D drawings or 3D models to Fuxingwang Hardware Products Co., Ltd. (Jiangmen Fuxingwang Hardware) for a free quotation and DFM feedback on your thread specifications.